Why Are Stud Welds on Galvanized Steel Sheet Not Strong?
Galvanized steel and Galvalume (aluminum-zinc coated steel) sheets are widely used in sheet metal fabrication due to their excellent corrosion resistance. However, during the stud welding process, many manufacturers encounter a common problem: the welded studs are not strong enough and may become loose or fall off.
This issue can directly affect product reliability, production efficiency, and final assembly quality.
So, why does stud welding on galvanized sheet metal fail? How can manufacturers improve welding strength?
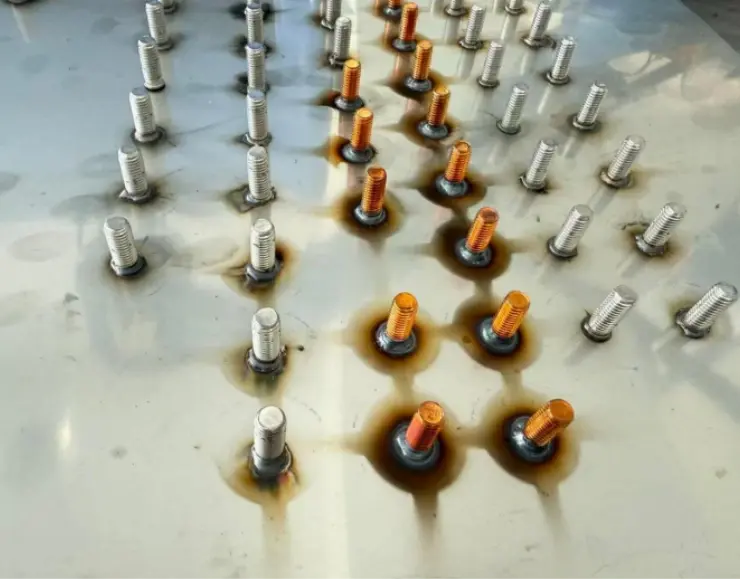
This article explains the main causes of weak stud welds on galvanized steel, key factors affecting welding quality, proper operating methods, and solutions for special applications.
1. The Main Reason Why Galvanized Steel Stud Welding Is Not Strong
The fundamental reason for weak welding on galvanized or Galvalume sheets is that the zinc coating or aluminum-zinc alloy coating prevents direct fusion between the stud and the base metal.
During the stud welding process, especially with capacitor discharge (CD) stud welding, a high current creates an instant arc between the stud and the workpiece.
However, zinc has a much lower melting point than steel:
- Zinc melting point: approximately 419°C
- Steel melting point: approximately 1538°C
When welding begins, the zinc layer melts and vaporizes quickly. If the zinc coating cannot be effectively removed from the welding area, several problems may occur:
- Porosity inside the weld joint
- Slag or impurities trapped in the welding zone
- Insufficient penetration
- Poor metallurgical bonding between stud and sheet metal
As a result, the stud may appear welded on the surface but actually has a weak connection, leading to false welding or stud detachment.
The key to achieving a strong stud weld is:
Remove the coating from the welding area through controlled arc action, allowing the stud material and base steel to form a direct metallurgical bond.
2. Key Factors Affecting Stud Welding Quality on Galvanized Sheets
The welding result depends on several factors, including material conditions, stud quality, operation method, and welding parameters.
2.1 Thickness of Zinc Coating on the Sheet Metal
The thickness of the galvanized layer directly affects welding performance.
A thicker zinc coating requires more welding energy to remove the coating effectively. If the welding energy is insufficient:
- The zinc layer may remain between the stud and steel sheet
- The weld pool cannot fully form
- Welding strength will decrease
Therefore, welding parameters should be adjusted according to different galvanized sheet specifications.
2.2 Stud Quality and Surface Condition
The quality of the welding stud also plays an important role.
High-quality welding studs usually have:
Copper Plated Surface
Copper plating improves:
- Electrical conductivity
- Arc stability
- Welding consistency
Proper Stud Tip Design
A slightly tapered stud tip helps:
- Concentrate the arc energy
- Improve ignition stability
- Promote zinc layer removal
- Increase penetration into the base material
Using inconsistent or poor-quality studs may cause unstable arcs and weak welds.
3. Correct Operating Methods for Strong Stud Welding
Even with a suitable welding machine and correct parameters, improper operation can still lead to welding failure.
3.1 Ensure Good Ground Connection
The grounding clamp must have a firm connection with the workpiece.
Poor grounding can cause:
- Unstable welding current
- Insufficient energy output
- Inconsistent weld quality
For reliable welding, it is recommended to use two grounding clamps and ensure they are tightly connected to clean areas of the workpiece.
3.2 Keep the Welding Gun Vertical
During stud welding, the welding gun should remain:
90° perpendicular to the workpiece surface
Incorrect angles may result in:
- Uneven pressure
- Uneven heat distribution
- Incomplete fusion
A vertical welding position ensures concentrated heat and stable welding pressure.
3.3 Adjust the Pre-Pressure and Lift Distance Correctly
The stud welding gun needs proper mechanical adjustment before welding.
Important settings include:
- Contact pressure
- Lift distance
- Stud positioning
Correct settings ensure:
- Stable arc initiation
- Full contact between stud and sheet metal
- Consistent weld penetration
4. How to Set Welding Parameters for Galvanized Steel Stud Welding?
Because the zinc coating consumes part of the welding energy, galvanized sheets usually require different parameters compared with ordinary steel plates.
For example:
When welding an M5 stud, the welding voltage may need to be increased by approximately 20%–30% compared with standard carbon steel applications.
However, the exact setting depends on:
- Sheet thickness
- Zinc coating thickness
- Stud diameter
- Welding machine power
- Required welding strength
The best approach is to perform welding tests and gradually optimize parameters.
5. How to Check Whether the Stud Welding Is Qualified?
A visual inspectio
n alone cannot confirm welding strength.
A practical quality test is the destructive bending test.
A qualified weld should meet the following requirements:
✔ The stud bends but does not separate from the sheet
✔ The weld joint remains intact
✔ No obvious cracks appear around the welding area
✔ The back side of the sheet has no excessive deformation
After proper welding, additional grinding or surface treatment is usually unnecessary.
6. Solutions for Difficult Galvanized and Galvalume Sheet Applications
For some special applications, such as:
- Thick galvanized sheets
- Heavy zinc coatings
- Aluminum-zinc coated sheets
- High-strength structural components
Adjusting welding parameters alone may not completely solve the problem.
In these cases, additional surface treatment methods can be used.
6.1 Mechanical Zinc Removal
The simplest method is removing the coating before welding.
Common methods include:
- Grinding with an angle grinder
- Sandpaper treatment
- Manual polishing
Advantages:
- Low cost
- Easy operation
Disadvantages:
- Requires additional labor
- May damage surface appearance
- Lower production efficiency
6.2 Milling Process
For precision components, milling can be used to remove the coating from the welding area.
Advantages:
- Accurate coating removal
- Flat welding surface
- Better welding consistency
This method is suitable for products requiring high dimensional accuracy.
6.3 Laser Zinc Removal
Laser cleaning technology is becoming an advanced solution for high-end manufacturing.
By using high-energy laser beams, the zinc coating can be rapidly vaporized before welding.
Advantages include:
- High efficiency
- Small heat-affected zone
- No mechanical damage
- Excellent surface quality
It is especially suitable for industries requiring high appearance standards and automated production.
7.Choose the Right Stud Welding Equipment
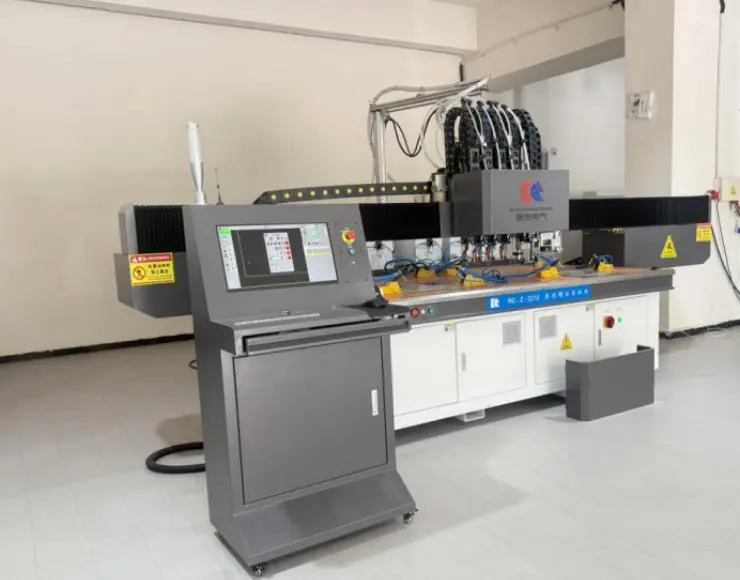
For galvanized sheet metal applications, the welding machine must provide:
- Stable discharge energy
- Accurate welding control
- Adjustable welding parameters
- Reliable arc performance
A professional capacitor discharge stud welding machine can significantly improve welding consistency and reduce problems such as weak welds, missing fusion, and stud falling.
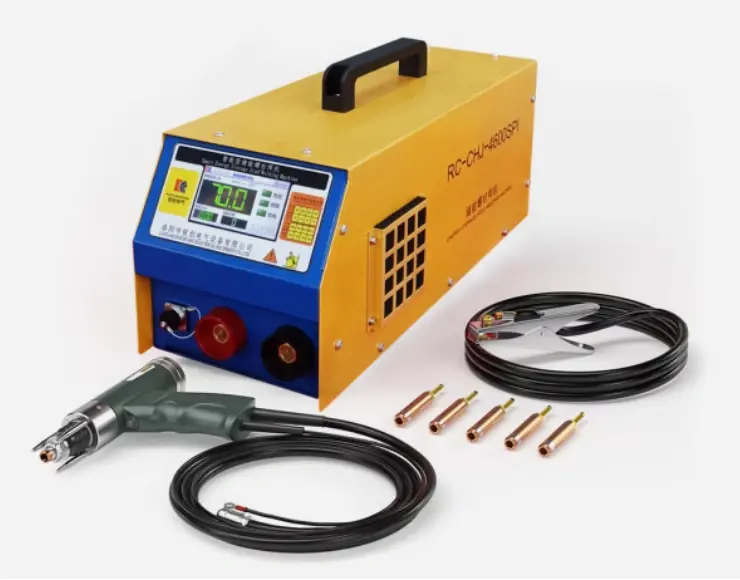
When selecting equipment, manufacturers should consider:
- Stud diameter range
- Material type
- Sheet thickness
- Production volume
- Automation requirements
Conclusion
Weak stud welding on galvanized steel sheets is mainly caused by the interference of zinc or aluminum-zinc coatings during the welding process.
To achieve strong and reliable welds, manufacturers should focus on:
- Selecting high-quality studs
- Ensuring proper grounding and gun positioning
- Optimizing welding parameters
- Removing coatings when necessary
- Choosing suitable stud welding equipment
With the correct process control and equipment selection, galvanized and Galvalume sheets can achieve strong stud connections while maintaining their excellent corrosion resistance.